Engineered Modular Compounds & Site Solutions
Explore our factory-prefabricated modular units engineered for rapid global export and severe sub-zero thermal performance across Canadian mining, energy, and infrastructure job sites.
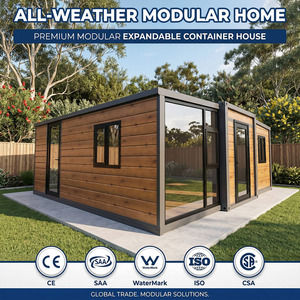
Expandable Modular Container Housing & Temporary Staff Villas
Turnkey expandable container units featuring integrated electrical distribution, pre-installed MEP systems, and sub-zero climate protection for remote camps.
Send an Inquiry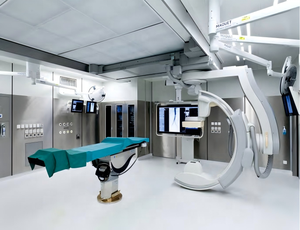
Modular Stainless Steel Container Clinic & Portable Hospital Lab
Medical-grade mobile healthcare modules built with medical cleanroom walls, HEPA filtration integration, and rapid site assembly features.
Send an Inquiry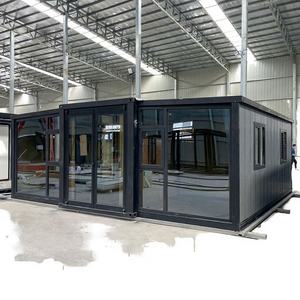
Portable Prefab Commercial Kitchen & Modular Dining Facilities
Scalable food service and mess hall modules constructed with fire-rated PUR sandwich panels, washable hygienic floors, and extraction ventilation.
Send an Inquiry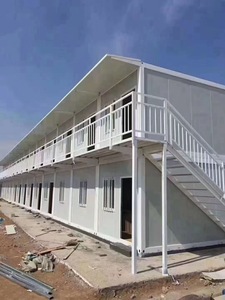
Two-Story Stackable Modular Compound & Field Operations Office
High-density structural steel site office configuration with internal staircase, high snow-load roof structural framing, and executive offices.
Send an Inquiry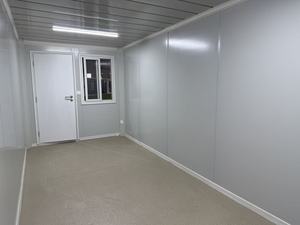
Z-Foldable Portable Site Office & Quick Storage Module
Ultra-compact logistics footprint allowing up to 10 units per flatbed truck, erecting in under 15 minutes per module with minimal crane operations.
Send an Inquiry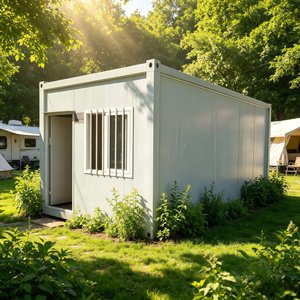
Custom Mobile Healthcare Shelter for Northern & Remote Operations
Insulated field triage unit designed for remote exploration camps, featuring autonomous generator tie-ins and dual HVAC climate controls.
Send an Inquiry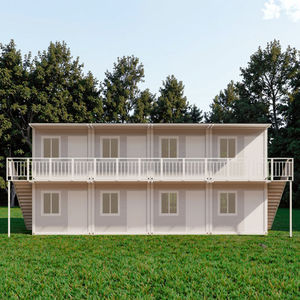
Modular Prefabricated Educational Buildings & Training Complexes
Spacious, bright modular educational units equipped with acoustic wall treatments, energy-efficient LED lighting, and commercial HVAC ducting.
Send an Inquiry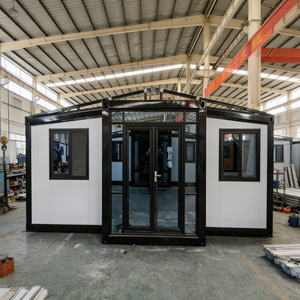
Heavy-Duty Steel Framed Expandable Medical & Command Post
Galvanized light gauge structural steel framework providing superior lateral seismic resistance and long-term anti-corrosion protection.
Send an InquiryEngineering Excellence in Canadian Site Compound Exporting
An authoritative analysis of technical specifications, cold-climate thermal dynamics, structural load engineering, and international supply chain optimization for modular infrastructure across North America.
Canadian Climate & Thermal Envelope Optimization
Deploying modular site compounds in Canada demands engineering precision tailored to severe climate zones—ranging from maritime humidity in British Columbia to extreme sub-zero permafrost conditions in northern Alberta, Northwest Territories, and Nunavut.
Our structural modular designs incorporate advanced thermal break technology, eliminates cold bridging through structural steel chassis, and utilizes continuous polyurethane (PUR) or polyisocyanurate (PIR) core sandwich paneling. Wall and roof assembly ratings exceed R-30 to R-40 insulation values, ensuring operational efficiency and occupant thermal comfort even during prolonged -40°C winter conditions.
Structural Snow Load & Wind Shear Engineering
Under the National Building Code of Canada (NBC), modular structures must meet strict structural criteria regarding ground snow loads ($S_s$) and rain loads ($S_r$).
Our engineered steel frames utilize cold-formed high-tensile galvanized steel profiles and custom hot-rolled structural steel columns capable of handling snow accumulation loads of up to 4.5 kPa (94 PSF) and basic wind velocity pressures exceeding 1.2 kPa. All factory welds adhere to rigorous international structural welding benchmarks (aligned with CWB standards), safeguarding structural integrity during trans-oceanic shipping and remote site cranes lifting.
Canadian Project Application Scenarios
How international EPC contractors, mining conglomerates, and infrastructure developers deploy our modular site compound exports across key Canadian economic sectors.
1. Alberta Oil Sands & Resource Extraction Workforce Camps
Energy developments in Fort McMurray and the Athabasca region require large-scale, self-contained workforce camps deployed on demanding timelines. Our modular compounds are integrated to form complete turnkey cities for up to 2,000 workers—featuring executive sleeping dormitories, commercial kitchen modules, recreation complexes, and central HVAC plant integration.
2. Mining Exploration Camps in Northwest Territories & Yukon
Operating in severe sub-arctic environments requires modular buildings that can be transported via ice roads or flat-pack container sea-freight. Our flat-pack and Z-fold container site offices provide rapid, low-weight assembly on elevated timber pads or helical screw piles to preserve underlying permafrost layers without permanent environmental disruption.
3. Clean Energy & Hydroelectric Infrastructure Projects in BC & Quebec
Large hydro dam construction and wind farm installations in coastal British Columbia or northern Quebec demand modular site compounds capable of resisting atmospheric moisture, high rainfall, and wind-driven rain. We engineer moisture-resistant vapor-permeable membrane wall layers and marine-grade epoxy steel paint coatings.
4. Modular Healthcare & Emergency Medical Stations for Remote First Nations Communities
Bridging healthcare accessibility gaps in remote northern communities demands rapidly deployable, ISO-compliant medical cleanrooms and primary care container clinics. Pre-fitted in our factory with electrical panels, plumbing manifold trunks, medical gas lines, and antimicrobial surface finishes, these units arrive operational upon site placement.
Canadian Modular Construction Trends & Export Dynamics
Key market drivers accelerating the shift toward imported factory-built modular compounds across Canadian procurement channels.
Domestic Skilled Labor Shortages
Canada’s acute labor shortage in trades across rural job sites has elevated the cost of stick-built remote construction. Importers leverage our off-site industrial manufacturing—where 85% of building assembly occurs in automated factory lines—reducing site labor costs by up to 60%.
ESG & Circular Economic Demands
Major Canadian natural resource companies operating under strict ESG frameworks require relocatable, reusable infrastructure. Our steel-framed modular compounds offer a 25+ year structural lifespan and can be demounted, transported, and reconfigured for subsequent project lifecycles with zero landfill waste.
Schedule Compression Demands
Short seasonal construction windows in northern regions demand ultra-fast site establishment. By manufacturing modular units concurrently while site clearing and foundation works occur, overall project schedules are compressed by 30% to 50%.
Why Global Importers Partner With Us
Direct manufacturer advantages: In-house architectural design, rigorous quality control, automated roll-forming, and ocean freight logistics to Canadian ports.
Integrated Engineering & Architectural Design
Our multidisciplinary engineering hub delivers full BIM/REVIT structural, architectural, and MEP modeling in-house. We provide comprehensive submittal packages—including structural load calculations, thermal performance simulations, and single-line electrical diagrams—supporting local Canadian engineering reviews (P.Eng. stamp readiness).
ISO Certified Quality Management System
Every modular compound unit is manufactured under audited ISO 9001:2015 Quality Management, ISO 14001:2015 Environmental Management, and ISO 45001:2018 Occupational Health and Safety standards. Material traceability reports, mill test certificates for steel, and factory acceptance testing (FAT) are provided prior to export dispatch.
Cost-Optimized Global Export Logistics
Strategically shipping from modern manufacturing hubs in Turkey, we utilize flat-pack packaging engineering that allows four standard demountable office container units to bundle into a single 40ft High Cube ISO shipping container. This cuts trans-Atlantic or trans-Pacific ocean freight costs by up to 75% compared to fully volumetric modular shipping.
Turnkey MEP Factory Integration
Plumbing trunks, concealed electrical wiring in rigid conduits, distribution boards, LED lighting arrays, and sanitary fixtures are pre-installed in the factory. Pre-testing of electrical insulation and pressure testing of water circuits before packing ensures immediate plug-and-play field utility hookup on site.
Canadian Procurement & Technical FAQ
Addressing common inquiries from Canadian procurement leads, general contractors, and import logistics specialists.
Our engineering team designs structural modular buildings to align with the National Building Code of Canada (NBC) requirements for structural strength, snow loads, wind loads, and thermal insulation. We collaborate with local Canadian Professional Engineers (P.Eng.) to review calculation packages, foundation interfaces, and stamped approvals. Electrical components (wiring, breaker panels, fixtures) are specified to meet CSA (Canadian Standards Association) or equivalent international standards required for Canadian customs clearance and site inspection.
We manage FOB, CIF, or DDP shipping to major Canadian ocean ports, including the Port of Vancouver (for Western Canadian mining/energy sites in BC and Alberta), the Port of Montreal, and the Port of Halifax (for Eastern and Atlantic projects). Flat-pack container bundles are transported via standard intermodal rail (CN or CP Rail) directly to inland terminals in Calgary, Edmonton, Winnipeg, or Toronto for final truck delivery to site.
To withstand harsh Canadian winters, our cold-climate modules feature high-density Polyurethane (PUR) or Polyisocyanurate (PIR) core sandwich wall and roof panels ranging from 80mm to 150mm in thickness. Combined with insulated floor assemblies, double-glazed low-E argon-filled PVC/aluminum windows, continuous EPDM weather gaskets, and thermal break structural steel interfaces, the buildings maintain low heat loss and prevent internal condensation.
Factory production for standard site compounds (e.g., 50 to 100 modular units) typically takes 3 to 5 weeks following engineering drawing sign-off. Ocean transit time from our export facilities to Canadian ports ranges between 20 to 30 days depending on the destination port (East Coast vs. West Coast). Overall door-to-door lead times average 8 to 11 weeks.
Yes. All flat-pack and containerized site compounds are engineered with structural corner castings and high-tensile steel frames specifically designed for repeated lifting, demounting, flat packaging, and transport. A 100-man accommodation camp can be dismantled, packed into container bundles, and relocated to a new mining lease or infrastructure site without structural degradation.
We provide comprehensive installation manuals, foundation load drawings, step-by-step 3D assembly video tutorials, and dedicated factory technical supervisors who can be dispatched on-site to guide local Canadian erection crews, ensuring fast, compliant, and safe modular camp setup.
Ready to Engineer Your Canadian Site Compound?
Consult with our senior modular engineers today for detailed technical specifications, CAD layout planning, budget quotes, and door-to-door logistics schedules for your Canadian project.